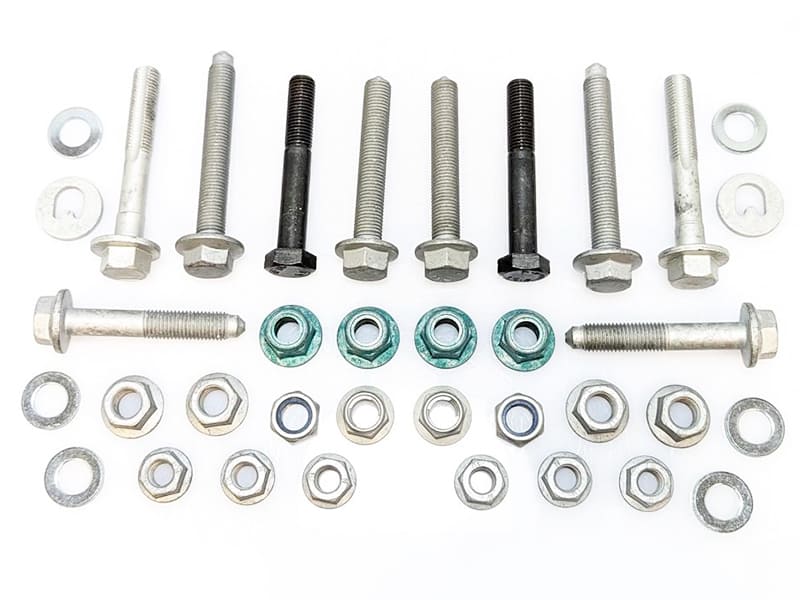
Mechanical threads are often found in screws, bolts, and other fasteners and are an important component of mechanical and structural integrity. Using the right mechanical threads can improve structural stability, allow assemblies to be assembled accurately, be adjustable, and easy to maintain, making them widely used in industries ranging from aerospace and automotive to construction and manufacturing.
What is a thread?
“Thread” refers to a helical ridge or groove on the surface of a cylindrical object, typically a screw, bolt, or nut. Threads are designed to provide a way for these objects to join together by engaging with each other in a rotational motion. Threads can be classified as either internal (on the inside of a cylindrical opening) or external (on the outside of a cylindrical surface).

threads_600x400
What are the key geometric parameters of threads?
- Pitch: The distance between corresponding points on adjacent threads. It is usually measured in millimeters (mm) or inches (in).
- Major Diameter (or Outer Diameter): The largest diameter of the threaded section for external threads or the smallest diameter for internal threads.
- Minor Diameter (or Root Diameter): The smallest diameter of the threaded section for external threads or the largest diameter for internal threads.
- Crest: The top surface of an external thread or the bottom surface of an internal thread.
- Root: The bottom of an external thread or the top of an internal thread.
- Flank: The surface connecting the crest and root of a thread.
- Thread Angle: The angle formed by the intersection of the flanks. It is typically 60 degrees for standard metric threads and 55 degrees for standard imperial (UNC/UNF) threads.
- Lead: The axial distance the thread advances in one complete turn.
- Thread Height: The distance between the crest and root of the thread.
- Pitch Diameter: The theoretical diameter at which the thread thickness is equal to the space between threads. For an external thread, it lies between the major and minor diameters; for an internal thread, it lies within the minor diameter.

geometric_parameters_of_threads_600x400
What are the tools for identifying threads?
-
Thread Pitch Gauge:
A thread pitch gauge helps determine the pitch (distance between threads) of a threaded object. It consists of a set of blades with known thread pitches. By matching the threads with the blades, you can identify the pitch of the threaded part.

-
Thread Gauge:
Thread gauges are precision tools designed to check the accuracy of threads. They include go/no-go gauges for checking the correctness of thread dimensions, ensuring that the threads conform to specific standards.

-
Calipers:
Digital or manual calipers can be used to measure the major and minor diameters of threaded parts. This information, along with the pitch, helps identify the type of thread.

-
Micrometer:
Micrometers provide precise measurements of thread diameters. They are especially useful for measuring small-diameter threads with high accuracy.

-
Thread Measuring Wires:
These are used with a micrometer to measure the pitch diameter of a thread accurately. The wires are placed on either side of the threaded part, and the micrometer measures the effective diameter.

-
Go/No-Go Rings and Plugs:
– These are specially designed gauges for checking the accuracy of external (rings) and internal (plugs) threads. If the part fits the “go” gauge but not the “no-go” gauge, it indicates the thread is within acceptable tolerance.


-
Thread Identification Chart:
– Reference charts that provide information about common thread sizes, pitches, and other parameters. These charts can be used to visually match the characteristics of a thread.
-
Optical Comparators:
– Sophisticated tools that use optical magnification and comparison techniques to inspect and measure threads accurately.
-
Thread Files:
– These files have teeth designed to match specific thread pitches. By gently filing a threaded part, you can determine the pitch by the way the file engages with the threads.
-
Ultrasonic Measurement Devices:
– Advanced tools that use ultrasonic waves to measure thread dimensions non-destructively.
How to identify thread type?
Identifying thread types involves examining various characteristics of the threads, such as pitch, diameter, and shape. Here’s a step-by-step guide on how to identify thread types:
-
Measure the Thread Pitch:
Use a thread pitch gauge to measure the distance between threads. Match the threads to the blades on the pitch gauge. The pitch is a critical parameter in identifying thread types.

-
Determine the Diameter:
– Measure the major and minor diameters of the threaded part using calipers or a micrometer. The major diameter is the largest diameter for external threads and the smallest for internal threads.

thread guage measurement 600×400
-
Count the Threads:
– Count the number of threads per inch (TPI) for imperial threads or threads per millimeter (TPM) for metric threads. This information can help narrow down the possibilities.
-
Check Thread Form:
– Examine the shape of the thread. Threads can be triangular (V-shaped), square, or rounded. The thread form, along with pitch and diameter, helps identify the thread type.
-
Use Reference Charts:
– Consult thread identification charts that provide information on common thread types. These charts typically include details on pitch, diameter, and thread form for various thread standards.

types_of_thread_600x400
-
Compare with Known Standards:
– Compare the measured parameters (pitch, diameter, and thread form) with known standards for threads. This includes standards such as ISO metric threads, Unified National Coarse (UNC), Unified National Fine (UNF), and others.
-
Inspect the Thread Angle:
– Measure the angle between the thread flanks. Standard thread angles are commonly 60 degrees for metric threads and 55 degrees for imperial threads. Unusual angles may indicate a non-standard thread type.

-
Use Specialized Tools:
– Employ specialized tools like thread gauges, thread files, or optical comparators for more accurate measurements. These tools are designed to aid in identifying thread types with precision.
What are the thread standards?

There are several thread standards used globally, each designed for specific applications and industries. Here are some of the commonly recognized thread standards:
-
ISO Metric Threads:
– These threads follow the International Organization for Standardization (ISO) metric thread standard. They are widely used in countries that have adopted the metric system. ISO metric threads have a 60-degree thread angle.
-
Unified Thread Standard (UNC, UNF):
– The Unified Thread Standard, established by the United States, includes two main series: UNC (Unified National Coarse) and UNF (Unified National Fine). UNC has fewer threads per inch, while UNF has more threads per inch. Both have a 60-degree thread angle.
-
British Standard Whitworth (BSW) and British Standard Fine (BSF):
– These are historical thread standards once widely used in the United Kingdom and other British-influenced regions. BSW has coarser threads, while BSF has finer threads.
-
National Pipe Thread (NPT):
– NPT is a U.S. standard for tapered threads used in pipe and fittings. It is common in plumbing and pipe applications. NPT threads have a taper of 1:16 and a 60-degree thread angle.
-
National Pipe Thread Tapered (NPTF):
– Similar to NPT, NPTF is a U.S. standard for tapered pipe threads but with a modified crest to improve sealing. It is often used in applications where a leak-tight seal is critical.
-
Acme Threads:
– Acme threads have a trapezoidal shape and are commonly used in lead screws and other power transmission applications. The Acme thread form provides efficient sliding motion.
-
Buttress Threads:
– Buttress threads have one flank that is perpendicular to the axis and another that is inclined. They are often used in applications where a large axial force is applied in one direction.
-
Unified Miniature Screw Threads (UNM):
– This is a thread standard for miniature screws, often used in electronics and small mechanical components.
-
JIS Metric Threads:
– Japan Industrial Standards (JIS) metric threads are used in Japan. They are similar to ISO metric threads but may have some variations.
-
Metric Fine Threads:
– In addition to the standard ISO metric threads, there are finer pitch variations used in certain applications that require a higher level of precision.
What are the common thread types?
There are several types of threads, each designed for specific applications and requirements. Here are some common types of threads:

-
V-Threads:
These are standard triangular threads with a 60-degree thread angle, commonly used in metric and Unified National Coarse (UNC) threads.
-
Square Threads:
Square threads have a square-shaped profile and are often used in applications where high efficiency in transferring motion is required. They are commonly found in lead screws.
-
Acme Threads:
Acme threads have a trapezoidal profile and are used in applications where efficient sliding motion and high load-carrying capacity are important. They are commonly used in lead screws, jacks, and clamps.
-
Buttress Threads:
Buttress threads have one flank that is perpendicular to the axis and another that is inclined. They are used in applications where a large axial force is applied in one direction, such as in vices and jacks.
-
Knuckle Threads:
Knuckle threads have a rounded profile and are used in applications where a smooth, continuous engagement is desired, such as in some types of couplings.
-
Whitworth Threads:
Whitworth threads were historically used in the United Kingdom and have a 55-degree thread angle. They are less common today but may still be found in older equipment.
-
Unified Threads:
Unified threads include both Unified National Coarse (UNC) and Unified National Fine (UNF) threads. UNC has fewer threads per inch, while UNF has more threads per inch. They have a 60-degree thread angle.
-
Pipe Threads (NPT and NPTF):
National Pipe Thread (NPT) and National Pipe Thread Tapered (NPTF) are used for tapered pipe threads in plumbing and other pipe applications. NPTF has a modified crest for improved sealing.
-
Metric Threads:
Metric threads follow the International Organization for Standardization (ISO) metric standard. They have a 60-degree thread angle and are widely used in countries that adopt the metric system.
-
Micro Threads:
Micro threads are extremely small threads used in miniature applications, such as electronics and medical devices. They have very fine pitches.
-
Truncated Threads:
Truncated threads have a portion of their profile removed to create a flat surface. This can be useful for certain applications where a flush finish is required.
Thread direction (left-hand and right-hand)
What are right-hand threads and left-hand threads ?

Right-hand and left-hand threads refer to the direction in which the threads on a screw, bolt, or other threaded fastener advance or retreat as they are rotated. The difference lies in the helical arrangement of the threads.
- Right-hand thread: In a right-hand thread, the thread slopes upward and to the right as viewed from the screw or bolt.
- Left-Hand Thread: In a left-hand thread, the thread slopes upward and to the left as viewed from the screw or bolt.
How to judge right-hand thread and left-hand thread?
Distinguishing between right-hand threads and left-hand threads can be done by observing the direction in which the thread advances when turned. Here are two common methods to determine whether a thread is right-hand or left-hand:
-
Visual Observation:
– Hold the threaded object vertically or horizontally, depending on the thread orientation.
– If the threads appear to slope upward from left to right, like the path of a right-handed screw, it is a right-hand thread.
– If the threads slope upward from right to left, resembling a left-handed screw, it is a left-hand thread.
-
Rotation Direction:
– Imagine turning the threaded object as if tightening a screw or bolt.
– If turning the object clockwise (when viewed from above) causes it to move away from you, it is a right-hand thread.
– If turning the object counterclockwise (anti-clockwise) causes it to move away from you, it is a left-hand thread.
Keep in mind that these methods are based on conventions for visual observation and rotation direction. In practical terms, the direction of thread rotation is a critical factor. In right-hand threads, turning clockwise (as viewed from above) tightens the connection, while in left-hand threads, turning counterclockwise tightens the connection.
What is the difference between external threads and internal threads?

external threads and internal threads 600×400
External threads and internal threads refer to the placement of threads on a threaded fastener or component. The main difference lies in whether the threads are on the outside or inside of the object. Here’s a breakdown of each:
-
External Threads:
– External threads are located on the outside surface of a cylindrical object, such as a bolt or screw.
– These threads are designed to engage with matching internal threads of another component, typically a nut or a threaded hole.
– The male part with external threads is often referred to as a bolt, screw, or male threaded stud.
-
Internal Threads:
– Internal threads are located on the inside surface of a cylindrical object, such as a nut or a threaded hole in a piece of material.
– These threads are designed to engage with matching external threads of another component, typically a bolt or screw.
– The female part with internal threads is often referred to as a nut, female threaded receptacle, or internally threaded hole.
What are blind holes and through holes?


Through Hole: Extends completely through the material, with openings on both sides.
Blind Hole: Does not extend through the entire material; it has a limited depth and typically opens on one side.
What are metric threads and UN threads called? What are the recommended tolerances for internal and external threads?
Metric threads and UN (Unified National) threads are two different thread standards, each with its own set of specifications. Here’s a brief overview:
Metric Threads:
Metric threads follow the International Organization for Standardization (ISO) metric standard. They are commonly used in countries that adopt the metric system.
Metric threads are designated by the nominal diameter and pitch. For example, M8x1.25 indicates a metric thread with an 8mm nominal diameter and a pitch of 1.25mm.
UN (Unified National) Threads:
Unified National threads, often simply referred to as UN threads, are a standard used in the United States and other countries that haven’t fully adopted the metric system.
UN threads include Unified National Coarse (UNC) and Unified National Fine (UNF) series, among others. UNC has fewer threads per inch (coarser pitch), while UNF has more threads per inch (finer pitch).
For recommended tolerances of internal and external threads, the International Organization for Standardization (ISO) provides standards for metric threads, and the American National Standards Institute (ANSI) provides standards for UN threads. Here are some general guidelines:
Metric Thread Tolerances (ISO Standards):
Internal Threads: Generally, the tolerance classes for internal metric threads are denoted by a letter such as 6H, 6G, 4H, etc.
External Threads: Generally, the tolerance classes for external metric threads are denoted by a number such as 6g, 6h, 4g, etc.
UN Thread Tolerances (ANSI/ASME Standards):
Internal Threads (UNC and UNF): Classes 1A, 2A, and 3A are commonly used for external threads.
External Threads (UNC and UNF): Classes 1B, 2B, and 3B are commonly used for internal threads.
It’s important to refer to the specific ISO or ANSI/ASME standards for detailed information on thread tolerances, as these standards provide precise specifications for different thread sizes and classes. The choice of tolerance class depends on the desired fit and application requirements. Tighter tolerances (e.g., 6H/6g) provide a closer fit, while looser tolerances (e.g., 4H/4g) allow for easier assembly but may have more play.
Metric thread

“Metric thread” refers to a thread standard that follows the International Organization for Standardization (ISO) specifications and is typically used in countries that use metric units (millimeters). Metric threads are widely used in mechanical and engineering design. These threads are usually marked by starting with “M” followed by a number and a letter indicating the diameter and pitch of the thread.
For example, “M8x1.25” means that the diameter of the thread is 8 mm and the pitch is 1.25 mm.
Here are some common metric thread sizes and markings:
- **M6x1.0:** Thread with a diameter of 6 mm and a pitch of 1.0 mm.
- **M10x1.5:** Thread with a diameter of 10 mm and a pitch of 1.5 mm.
- **M12x1.75:** Thread with a diameter of 12 mm and a pitch of 1.75 mm.
When using metric threads, design and manufacturing standards often refer to ISO standards to ensure consistency in size and quality. This helps achieve component interchangeability and system reliability.
Grade fit for metric threads
The fit of metric threads is determined by the tolerance classes defined in the ISO metric thread standards. These tolerance classes consist of a combination of numbers and letters and are used to specify the acceptable range of dimensions for both internal and external threads. The most common metric thread tolerance classes are denoted by a number for external threads and a letter for internal threads. Here are some commonly used metric thread tolerance classes:
For External Threads:
The tolerance classes for external metric threads are denoted by a number. Commonly used classes include 6g, 6H, 4g, etc. The number indicates the level of tolerance, where a lower number corresponds to a tighter fit.
For Internal Threads:
The tolerance classes for internal metric threads are denoted by a letter. Commonly used classes include 6H, 6G, 4H, etc. The letter indicates the level of tolerance, where a higher letter corresponds to a tighter fit.
For example:
**6g:** This is a standard tolerance class for external metric threads, providing a general-purpose fit.
**6H:** This is a standard tolerance class for internal metric threads, also providing a general-purpose fit.
The choice of tolerance class depends on the specific requirements of the application. Tighter tolerance classes (e.g., 4H/4g) provide a closer fit, suitable for precision applications, while looser tolerance classes (e.g., 6H/6g) allow for easier assembly but may have more play.
It’s essential to refer to the specific ISO standards (such as ISO 965-1 for dimensions and ISO 965-2 for tolerances) for detailed information on metric thread tolerances for different sizes and classes.
What is a unified (UN) thread?

Unified National (UN) threads refer to a standard series of threads used in the United States and some other countries. The UN thread standard was established to provide a unified system for thread design and specifications. The term “unified” emphasizes the goal of creating a standardized system that replaces the variety of thread forms that existed before its introduction.
The Unified National thread standard includes two main series:
-
Unified National Coarse (UNC):
UNC threads have fewer threads per inch (coarser pitch).
These threads are commonly used in applications where rapid assembly or disassembly is required, and fine precision is not critical.
-
Unified National Fine (UNF):
UNF threads have more threads per inch (finer pitch).
UNF threads are used in applications where higher tensile strength and finer adjustment are required.
The designations for UN threads typically include the series (UNC or UNF), followed by a number indicating the nominal diameter and a class designation indicating the fit and tolerance. For example, a thread designation might be “1/4-20 UNC 2A,” where:
– “1/4” is the nominal diameter.
– “20” indicates 20 threads per inch.
– “UNC” specifies the thread series (Unified National Coarse).
– “2A” indicates the class of thread fit, with “2A” being a standard fit for external threads.
The UN thread standard is widely used in various industries, including manufacturing, automotive, and aerospace. It provides a systematic and standardized approach to threading, facilitating interchangeability and compatibility of threaded components.
Thread Parameter Table
UN Thread Chart


Metric Thread Chart


UNS Thread Chart


NPT/NPS Thread Chart

BSPP/BPST Thread Chart

PG Thread Chart

What are some practical tips for choosing the right thread type?
Choosing the correct thread type is critical to ensuring the proper operation and integrity of your mechanical components. Here are some practical tips to help you choose the right thread type for your specific application:
-
Standardization:
– Use standard thread types wherever possible. Standards such as ISO Metric Thread or Harmonized National Thread provide sound specifications and promote interchangeability.
-
Consider strength requirements:
– Select a thread type that meets the strength requirements of your application. Coarse threads (UNC) generally provide greater strength than fine threads (UNF).
-
Thread engagement:
– Consider the level of thread engagement required for the application. Thicker threads generally provide more engagement, which is advantageous for applications that require a secure connection.
-
Easy to assemble and disassemble:
– Consider ease of assembly and disassembly, especially if maintenance or repairs are contemplated. Coarse threads (UNC) generally allow for faster assembly and disassembly.
-
Cost considerations:
– Consider overall costs, including materials, manufacturing and assembly costs. Sometimes, a more standard or off-the-shelf thread type may be more cost-effective.
-
Thread direction:
– Consider whether right-hand or left-hand threads are suitable for your application. In some applications, using a left-hand thread can prevent accidental loosening.
References
Thread —— From Wikipedia
What are the different types of threads for manufacturing? ——From hubs
FAQs
About the Author: Gavin Xia